Featured Architectural Hardware & Cabinetry Components
Standardized testing, tight dimensional tolerances, and high structural durability engineered for international brand distributors, furniture factories, and project contractors.
Engineering Integrity in Kitchen Cabinet Handle Manufacturing
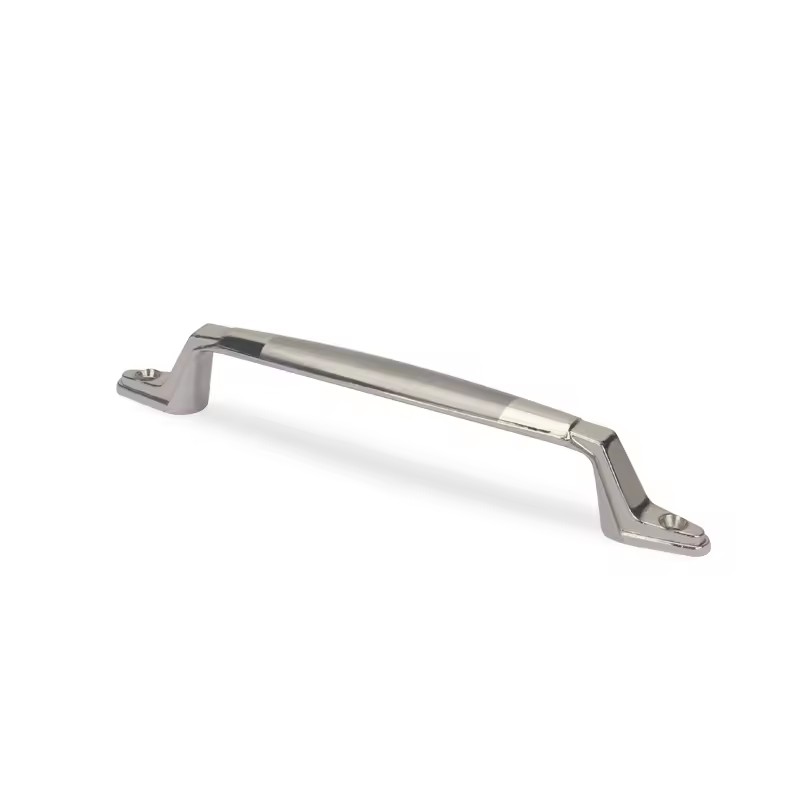
In high-humidity, high-traffic culinary environments, a cabinet pull handle is not merely an aesthetic trim—it is an ergonomic mechanical lever subject to continuous cyclic tension, acidic skin secretions, and chemical cleaning agents.
Zamak #3 / #5 Die-Casting
High-purity zinc alloy hot-chamber die casting eliminates micro-porosity and structural cavitation, producing dense substrates capable of supporting intricate neoclassical contours and deep structural recesses.
Tensile: 280-330 MPa6063-T5 Extruded Aluminum
Engineered for seamless architectural J-pulls, G-pulls, and continuous profile handles. Delivers superior linear straightness, micro-structural grain refinement, and thermal-treated impact resistance.
Anodic Oxide: ≥ 15μmSUS304 Austenitic Steel
Formulated with minimum 18% Chromium and 8% Nickel content to maintain a passivated chromium oxide exterior layer that prevents pitting and intergranular chloride stress cracking in professional kitchens.
Corrosion Class: C4/C5 MarineForged Solid C36000 Brass
Heavyweight architectural brass hot-forged at 750°C yields void-free molecular density. Preferred by bespoke millwork fabricators seeking living finishes, hand-burnished patinas, and antimicrobial tactile contact.
Density: 8.5 g/cm³| Substrate Material | Common Alloy Specs | Primary Surface Processes | Salt Spray Resistance (NSS) | Mechanical Tensile Pull Load | Ideal Architectural Application |
|---|---|---|---|---|---|
| Die-Cast Zinc Alloy | Zamak 3 / Zamak 5 | Multi-layer electroplating, PVD coating | 72 – 96 Hours (ASTM B117) | ≥ 450 N static force | Ornate, classic & transitional cabinet pulls |
| Extruded Aluminum | Alloy 6063-T5 / 6061 | Hard anodizing, matte powder coat | 96 – 120 Hours (ASTM B117) | ≥ 380 N static force | Minimalist edge profiles, Gola systems, linear pulls |
| Austenitic Stainless Steel | AISI 304 / 316 Grade | Fine satin brushing, vacuum PVD titanium | 168 – 240+ Hours (ASTM B117) | ≥ 750 N static force | Commercial catering, healthcare, coastal kitchens |
| Hot-Forged Brass | CuZn39Pb3 / C360 Brass | Clear electrophoretic lacquer, antiquing | 48 – 72 Hours (Passivated) | ≥ 600 N static force | Ultra-luxury residential joinery & heritage suites |
Future Procurement Trends in Cabinet Handles & Furniture Hardware
Commercial specifications are undergoing a paradigm shift driven by integrated European kitchen ergonomics, sustainable regulatory constraints, and advanced robotic manufacturing.
Integrated Linear Edge Profiles
Handle-less kitchen aesthetics continue to mature into continuous aluminum profile systems, inset lip handles, and recessed extrusion channels that merge flush with modern slab cabinetry doors.
Diamond Knurling & Tactile Textures
Precision CNC knurling (cross-hatch, straight linear, and herringbone patterns) introduces mechanical grip aesthetics, creating industrial luxury contrasts across matte black and brushed bronze finishes.
PVD Titanium Vapor Deposition
PVD replaces standard electroplating for premium projects, delivering nanoscale molecular bonding that resists abrasions, acidic fingerprints, ultraviolet discoloration, and harsh chemical cleaners.
Sustainable Closed-Loop Metallurgy
International compliance demands strict adherence to European RoHS, REACH, and circular economy regulations, prioritizing zero-lead zinc scrap, eco-certified trivalent chromium, and recyclable alloys.
How to Audit an Architectural Hardware Manufacturer
Mitigate container-level rejection risks by implementing rigorous B2B supplier verification across raw material certification, threading tolerances, and packaging integrity.
Tapping & Thread Durability
Inspect M4 and M6 screw hole depths and pitch consistency. Defective zinc castings suffer from micro-porosity and stripped threads under high-torque electric screwdriving. Top factories deploy cold-formed steel inserts or minimum 12mm thread depths with clean countersinking.
Spectrometric Metal Verification
Require XRF metal spectrum testing reports verifying virgin alloy composition. Substandard suppliers frequently blend unrefined post-consumer scrap into zinc alloy pots, introducing trace iron, lead, and cadmium that cause micro-cracking and galvanic corrosion over time.
Surface Adhesion & Hardness
Validate finish resilience through the cross-hatch tape test (ASTM D3359 Class 4B/5B) and the pencil hardness test (≥ 2H-4H). Handles must show zero delamination after exposure to boiling water immersion cycles and 5% neutral salt mist chambers.
Guangzhou Jarkul Hardware Advantage for Global Importers
Established in 2011 in Guangzhou, Guangdong, Guangzhou Jarkul Hardware Co., Ltd. serves tier-one cabinet hardware brands, building material distributors, and project developers in over 30 countries.
Documented Quality & SGS Verification
Every production run adheres to strict international testing standards. We provide buyers with documented proof of manufacturing compliance:
- Third-party SGS material, tensile, and corrosion test reports.
- Onsite verified supplier status with over 15 years of proven trade records.
- Multi-stage incoming raw material and finished packaging quality control.
- Pre-shipment batch sample archiving for traceability.
Full-Container Consolidation
Dramatically reduce landed logistics overhead by consolidating your complete furniture hardware bill of materials inside a single shipping container:
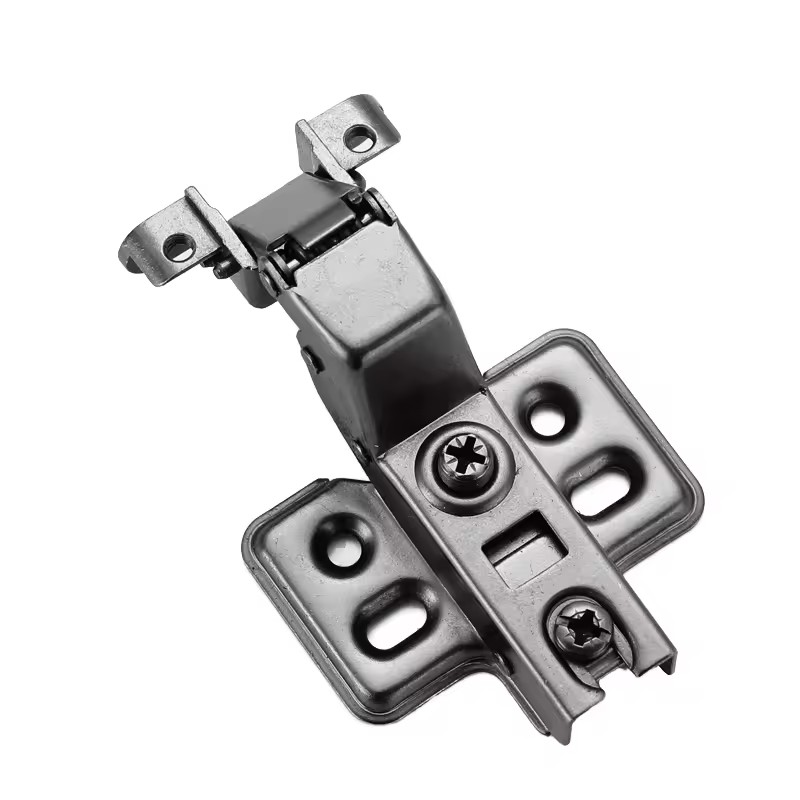
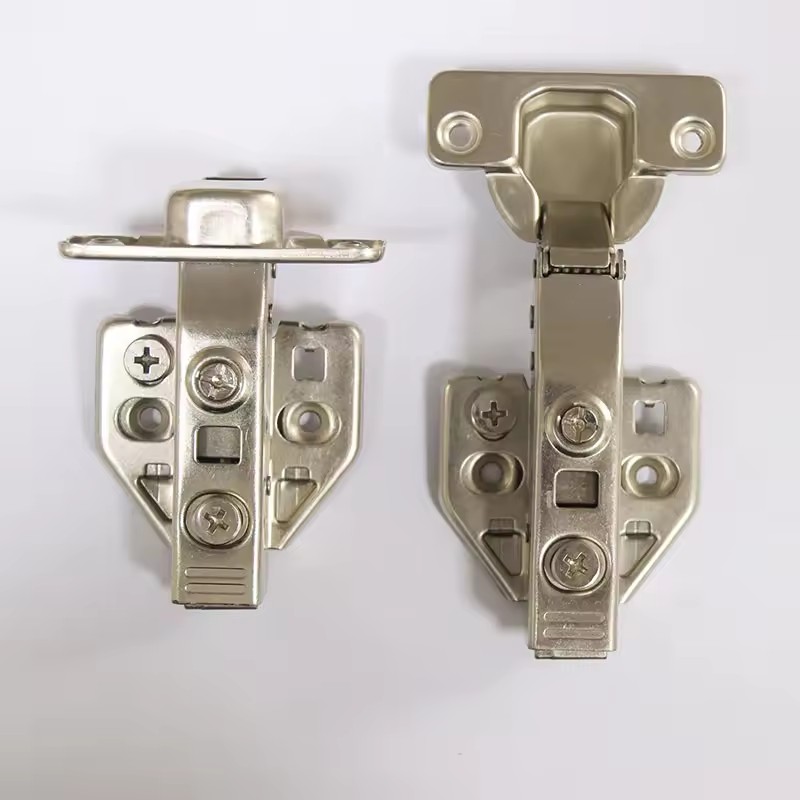
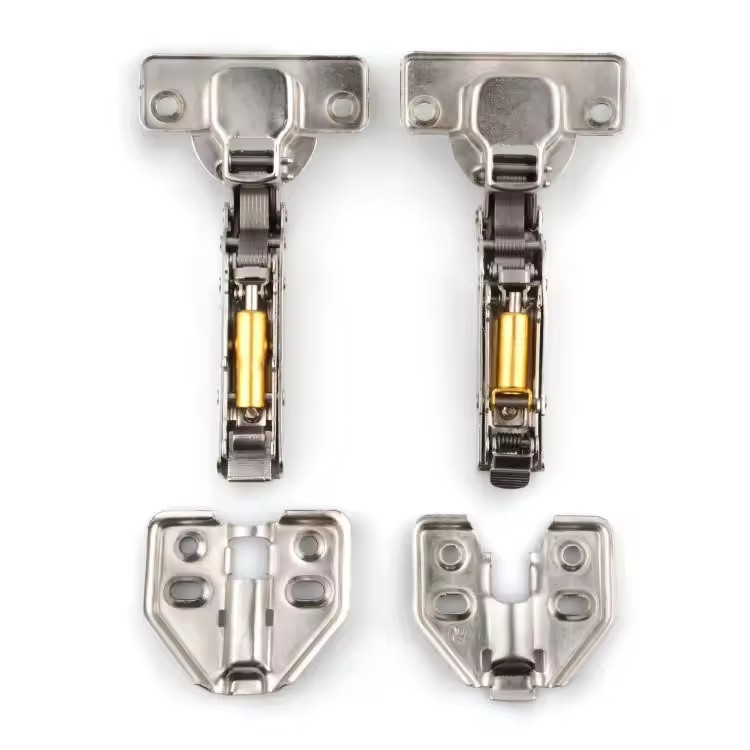
- Mix zinc and aluminum cabinet pulls with concealed soft-close hinges.
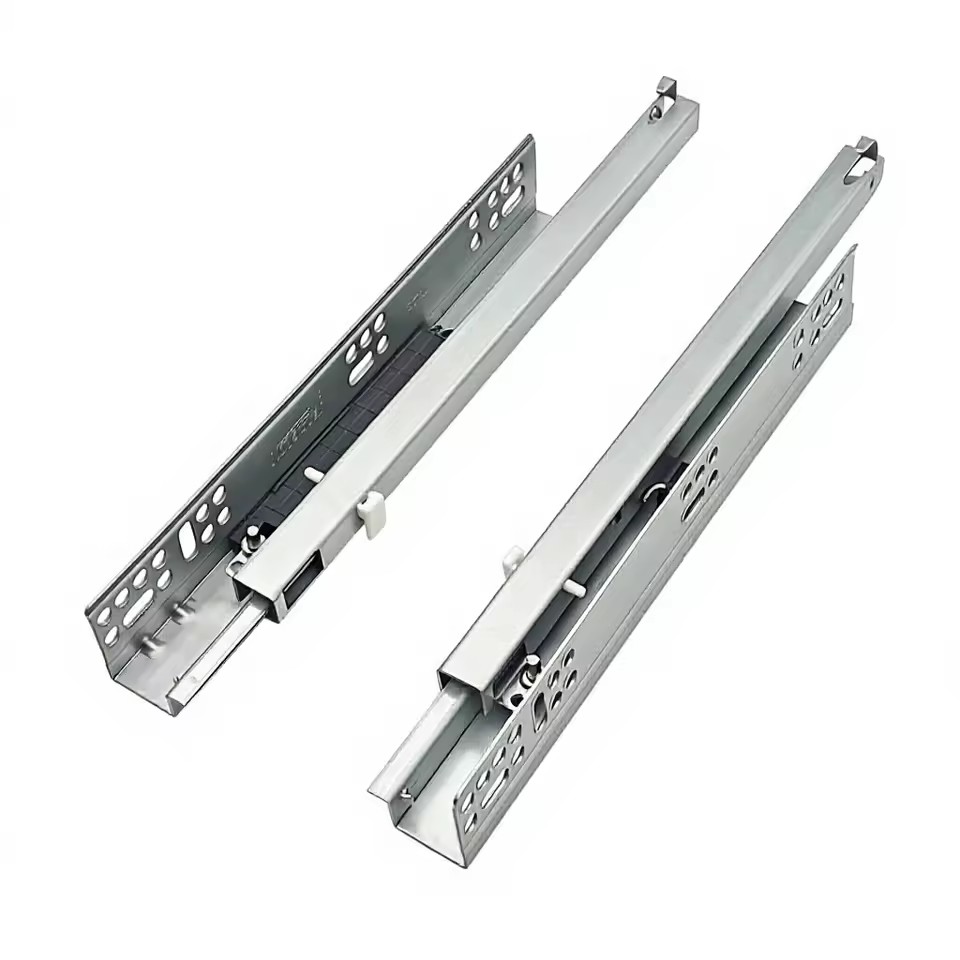
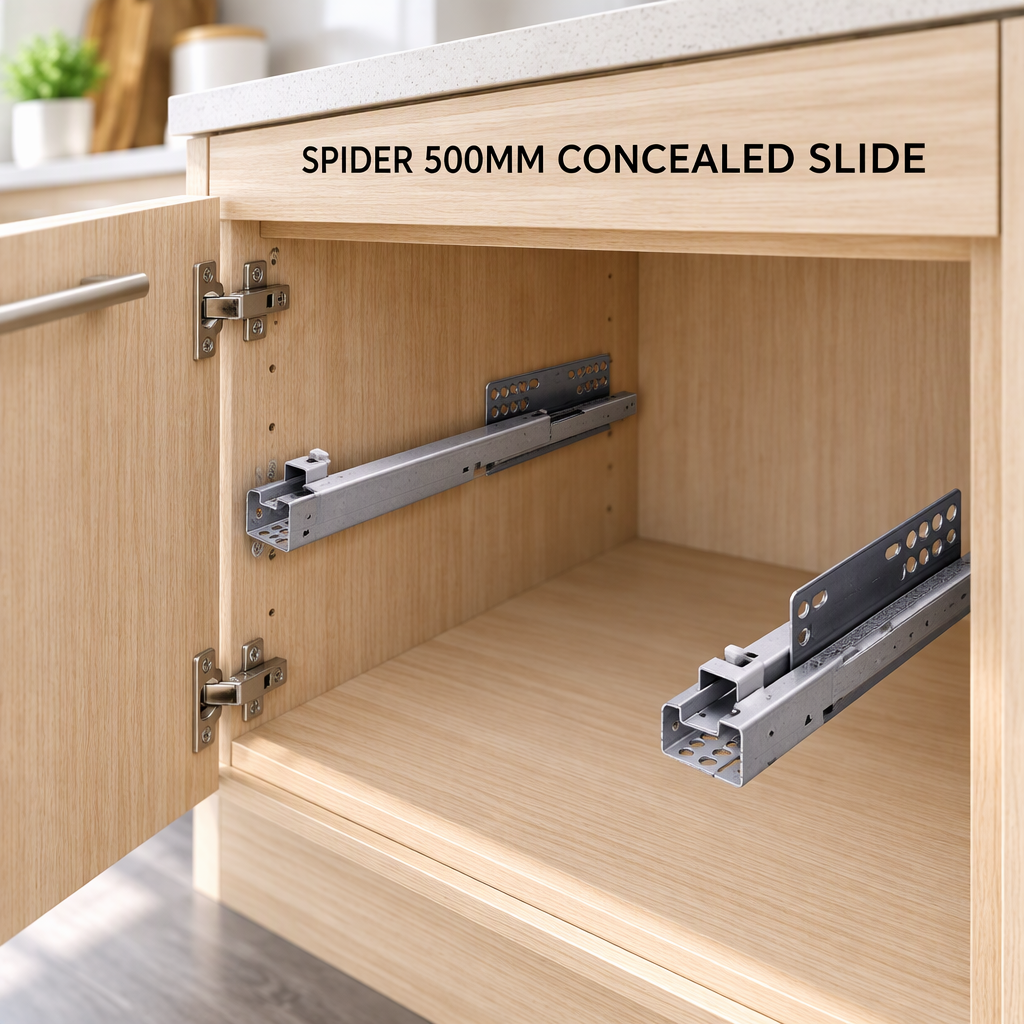
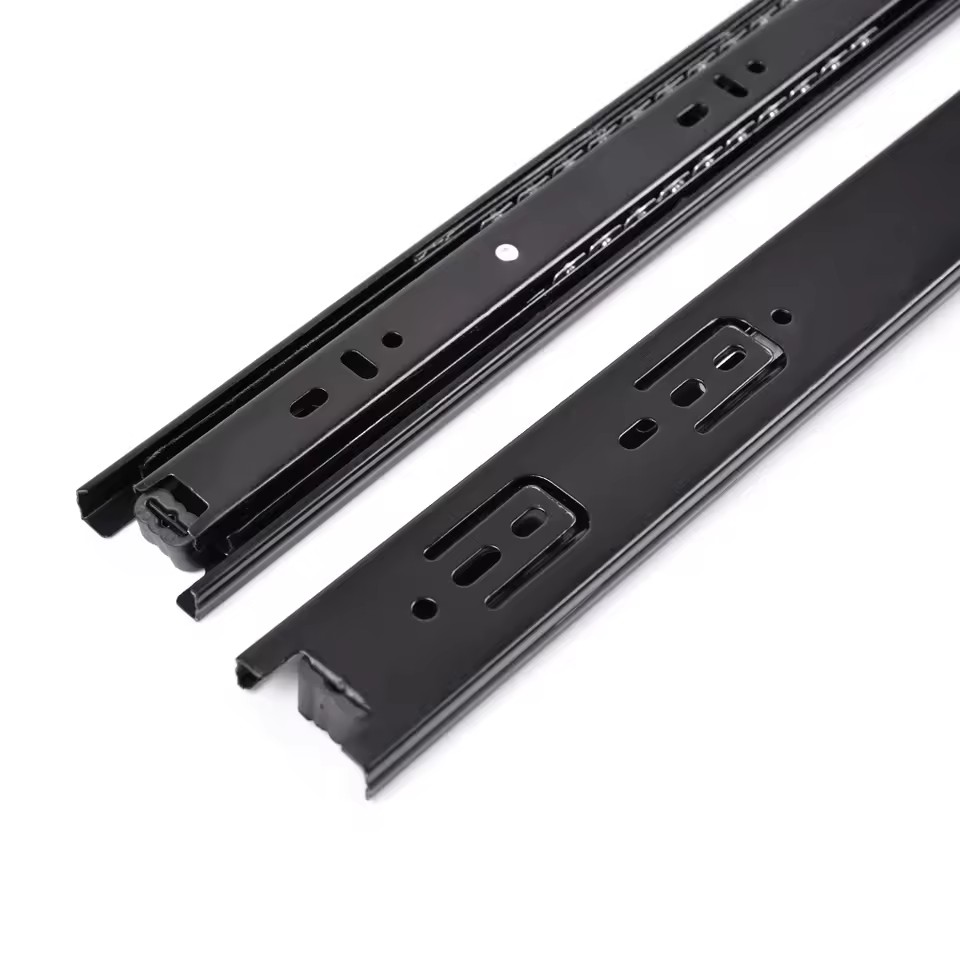
- Combine undermount runners and ball bearing drawer slides.
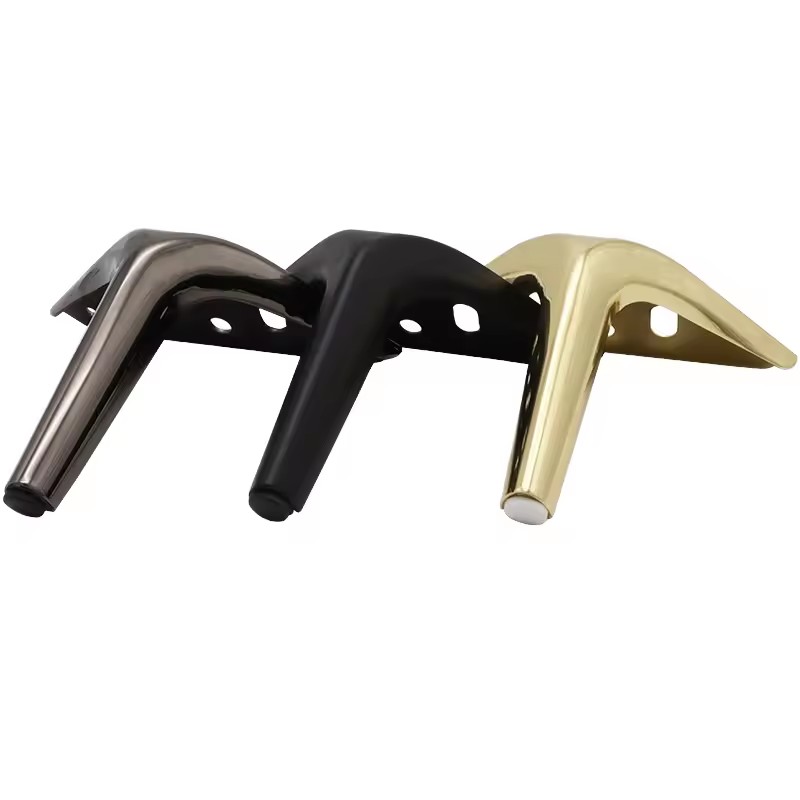
- Add hydraulic gas struts, wardrobe sliding dampers, and cabinet legs.
- Direct export documentation through Guangzhou, Huangpu, and Nansha ports.
OEM / ODM Custom Engineering
Transform architectural drawings into high-volume manufactured realities with dedicated mold engineering and private-label packaging:
- Custom tooling development with 15–25 day rapid sampling turnarounds.
- Laser-etched logo branding and customized hardware retail polybags.
- Drop-tested five-ply master cartons engineered for palletized container transit.
- Full flexibility across FOB, CIF, EXW terms with flexible payment frameworks.
Frequently Asked Questions by Global Hardware Importers
Critical answers regarding minimum order quantities, manufacturing tolerances, custom finishes, and shipment schedules.
The international 32mm system governs our handle tooling. Standard hole centers include 96mm, 128mm, 160mm, 192mm, 224mm, 256mm, and 320mm. For large appliance pulls and wardrobe doors, custom extrusion pulls up to 1000mm–1200mm are precision cut and tapped according to client CAD drawings.
For standard catalog finishes (such as Matte Black and Brushed Nickel on existing tooling), our MOQ starts at 1,000 to 2,000 pieces per size. For custom custom-tooled designs requiring new die-cast molds or custom anodized color matching, the standard production threshold is typically 3,000 to 5,000 pieces.
Yes. Every handle includes individually bagged M4 truss-head machine screws. Standard orders include 22mm or 25mm length screws for standard 18mm board thicknesses. We can also provide breakaway segment screws (20mm to 45mm adjustable) or custom lengths up to 50mm for double-thickness drawer fronts.
Every individual handle is encapsulated inside a high-clarity EPE foam sleeve or scratch-resistant sealed polybag alongside its screw packet. The products are systematically nested inside reinforced inner boxes, which are then packed inside heavy-duty 5-ply export master cartons and shrink-wrapped onto pallets.
Standard mass production lead time is 30 to 40 days following deposit verification and physical sample approval. For recurring contract orders with scheduled container call-offs, buffer inventory can be staged at our Guangzhou warehouse facility for expedited 10-day container stuffing.
We support international commercial trade terms including FOB Guangzhou / Shenzhen, CIF, CFR, and EXW. Payment terms include Telegraphic Transfer (T/T with 30% advance deposit and 70% against Bill of Lading copy), Irrevocable Letters of Credit (L/C at sight), D/P, D/A, and Western Union in USD, EUR, or CNY currencies.
Optimize Your Hardware Supply Chain with Direct Factory Pricing
Whether you are sourcing custom aluminum profiles, zinc die-cast pull handles, hydraulic soft-close hinges, or full-extension drawer runners, our Guangzhou engineering team provides complete technical CAD drawings, physical sample kits, and optimized container loading plans within 2 hours.